Oct 20, 2026Quality Control
Client case study: cost/defect reduction via drive style or finish change
cost/defect reduction via drive style or finish change
Background
Customer: Tier-1 manufacturer in appliances & outdoor equipment.
Objective: Reduce rework and warranty risk without changing major tooling.
Constraints: Keep existing hole specs and torque strategy where possible; no new capital equipment on the line.
Case A — Drive style change (Phillips → Torx six-lobe)
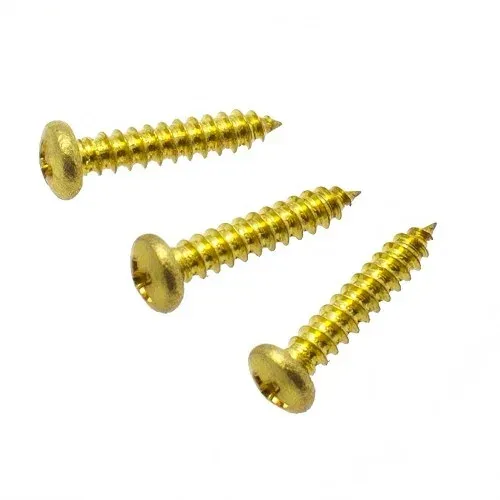
Original: Phillips pan head, zinc-plated steel, assembly torque 2.3–2.6 N·m.
Observed issues: Cam-out under power tools; cosmetic scratches near the head; periodic bit replacement causing micro-stoppages.
Intervention:
Switched to Torx (six-lobe) wafer head with same thread and material.
Verified with line trials: same torque window; new bits added to kitting.
No changes to hole size, pilot, or clamp stack.
Results (8-week comparison):
Cam-out events: ↓ 72% (per 10,000 insertions).
Rework on station: ↓ 41% (mainly cosmetic rejects).
Bit life: ↑ 28% before changeover.
Cycle time per unit: ↓ 6–8% on the two busiest stations.
Operator feedback: “Tool engagement is more positive; less pressure needed to hold the bit on-axis.”
Case B — Finish change (black oxide → zinc-nickel for outdoor use)
Original: Alloy-steel hex flange bolts with black oxide + oil on a bracket exposed to humidity and fertilizers.
Observed issues: Surface corrosion spots in field returns; occasional torque variability after storage.
Intervention:
Moved to zinc-nickel (12–15 µm) with trivalent passivation.
Maintained same grade and dimensions; added clear labeling for finish to avoid mixing.
Results (4-week pilot + 12-week rollout):
Salt-spray performance (lab): > 720 h to red rust (vs. < 96 h typical for black oxide).
Field returns (early read): ↓ ~60% for corrosion-related claims.
Torque consistency after 90-day storage: Improved; fewer outliers during fastening audits.
Measured impact (combined)
Defect rate (station level): from 1.6% → 0.6%.
Unplanned stoppages: ↓ 25–35% (bit change & rework).
Total applied cost per unit on the affected sub-assembly: –4.2% (materials slightly up; labor/rework/warranty down).
Quote (with permission): “Small spec changes—right drive, right finish—cut the noise on our line without new fixtures.” — Manufacturing Engineering Manager
Why it worked
Right drive for power tools: Torx six-lobe reduces cam-out and operator force, protecting finishes and bits.
Finish matched to environment: Zinc-nickel’s corrosion resistance outperforms black oxide in humid, chemical-exposed use.
Practical checklist for similar projects
Define the pain: cam-out logs, rework photos, torque histograms.
Pick the lever: drive style (Phillips/Pozi/Hex/Torx) or finish (zinc, zinc-nickel, HDG, black oxide, stainless).
Run a line trial: same torque window and tools where possible; compare cycle time and defects.
Lock the spec: head/drive, coating thickness, passivation, and packaging labels to avoid mixing.
Monitor 8–12 weeks: track rework, bit life, field returns.
About Hextro
Hextro Global Engineering Ltd. supplies screws, bolts, nuts, washers, shafts, pins, CNC turning parts, and aluminum/zinc die-castings with AQL-based inspection, clear documentation, and fast RFQ response.
Contact: inform@hextroco.com +86 137 2355 8561 · hextroco.com